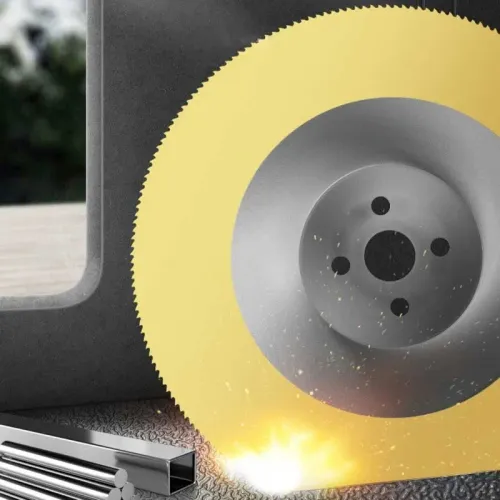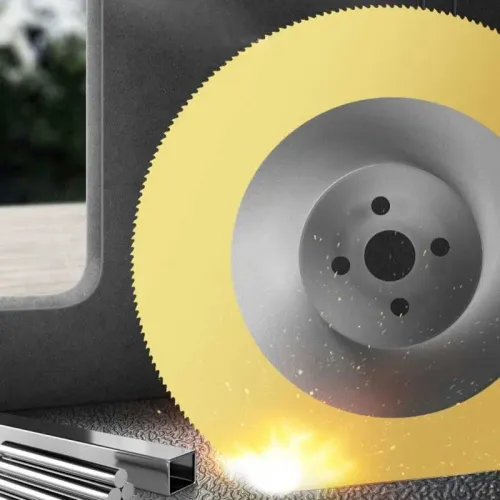
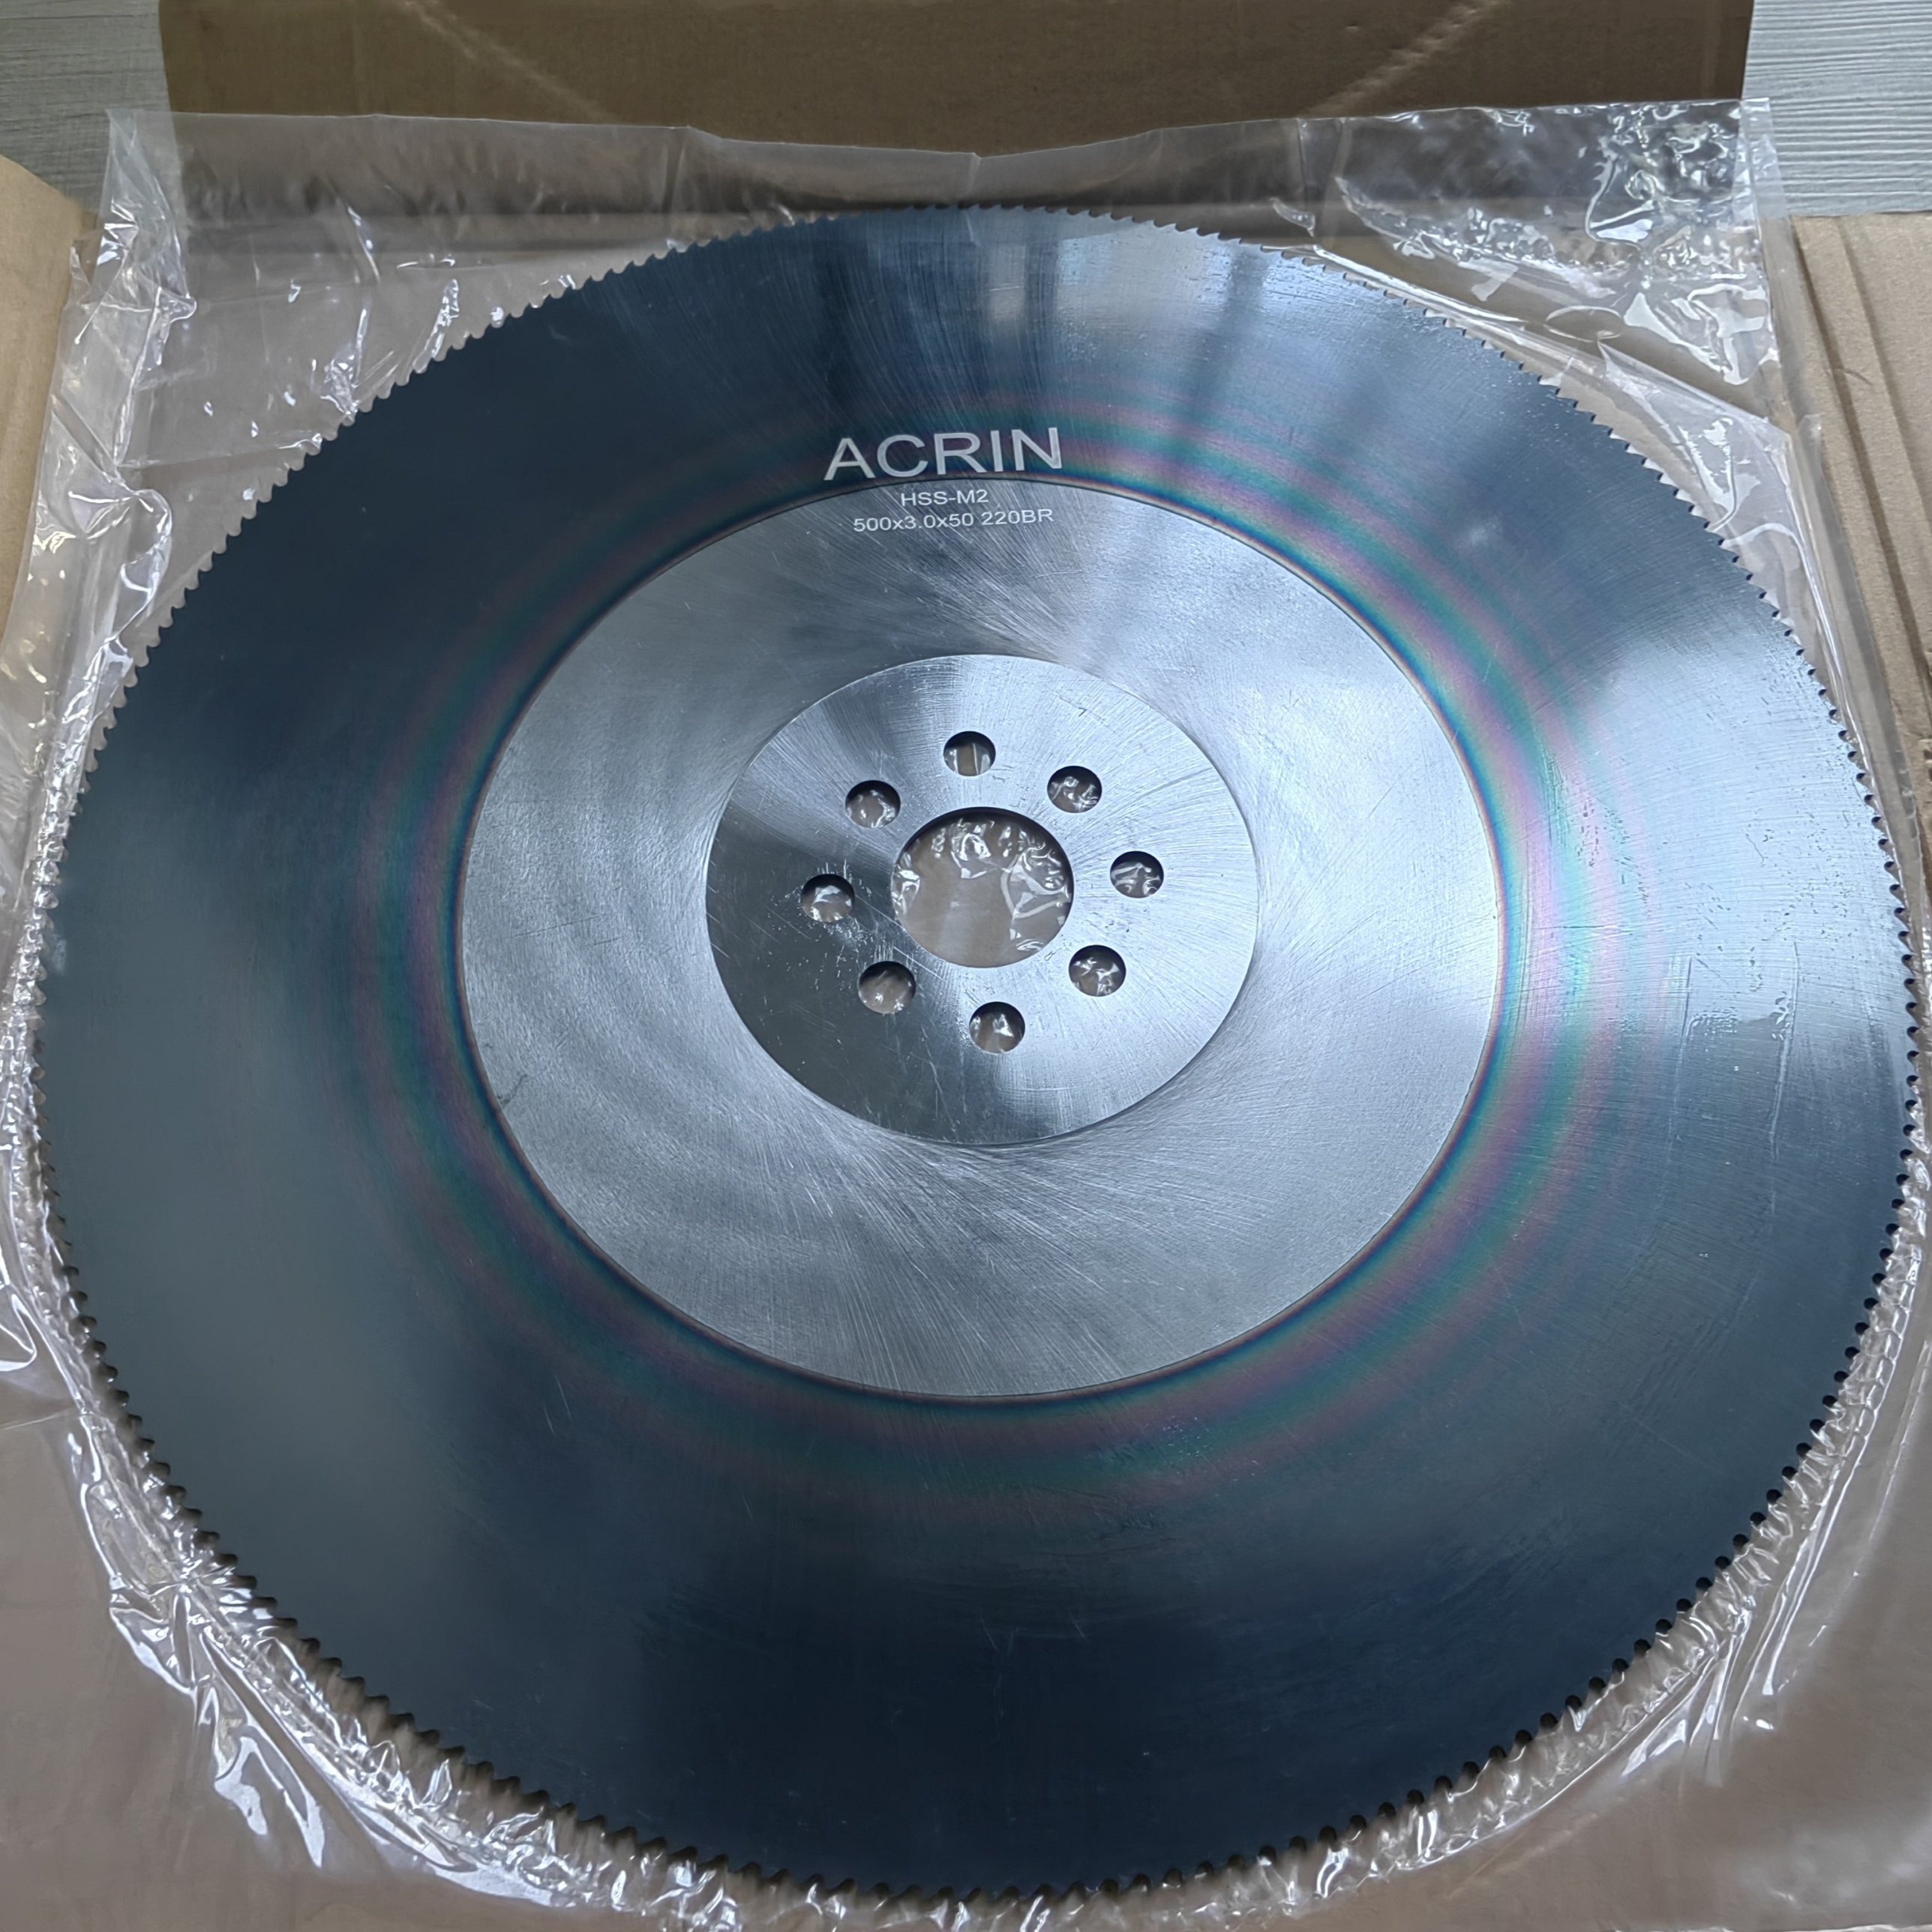
Burrs on cut pipes mean extra finishing work. These steps usually fix burr problems.
• Use a sharp blade and resharpen on time
• Match tooth count to the wall thickness
• Correct feed, steady clamping and good coolant
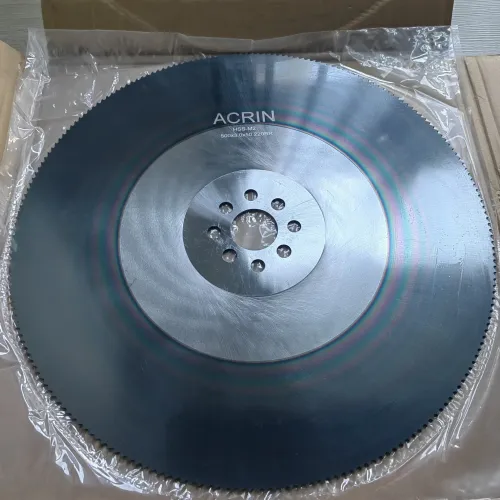
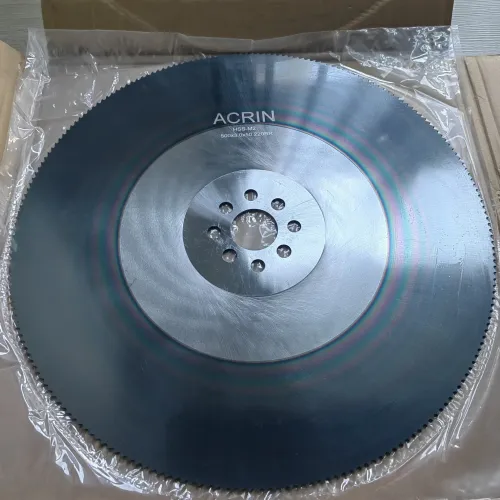
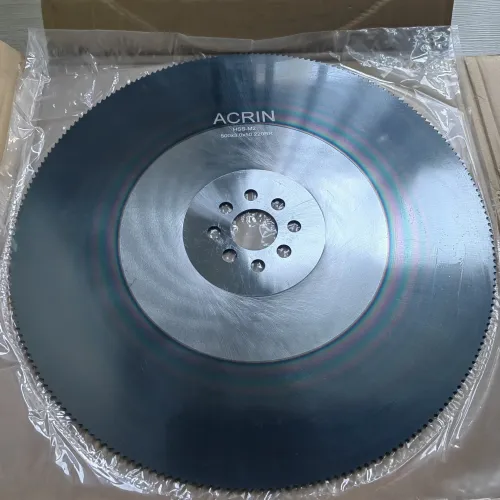
KWI HSS saw blade range:
Sizes: 275, 300, 350, 400, 450, 500 mm
Thickness: 1.2, 1.6, 2, 2.5, 3 mm
Bore: 32, 40, 50 mm
Teeth: 180, 200, 220, 240, 260
Profiles: BW and BR
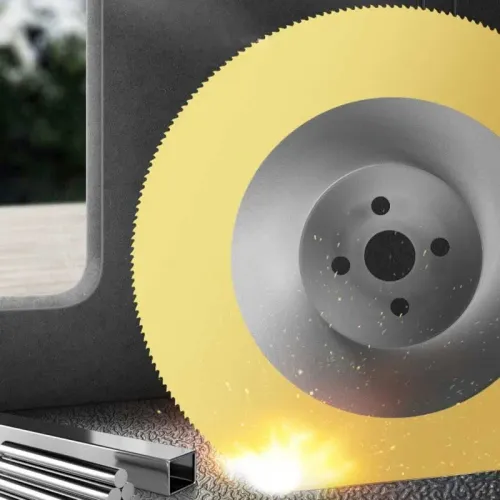
Coatings: steam, TiN, TiCN, TiAlN
Call 9625794957 or 7428410455 for a quote. Send your machine model, blade size, material and pipe size.
#KhandelwalIndustries #KWI #HSSSawBlade #PipeCuttingBlade #BurrProblemInPipeCuttingSolution
Keywords